Durability and efficiency in a single machine
Historically, the most robust machines sacrificed efficiency and the most efficient ones were not prepared for demanding conditions. The technological challenge was to bring both concepts together in a single solution: that is VITTA.
87.6%
Hydraulic efficiency measured on a certified test bench
86%
Efficiency measured under real operating conditions
70 bar
Working pressure · depths of up to 700 m
AISI 316
Super duplex
The two materials in the range, both investment cast
01
Optimised internal design
Three years redesigning the inside of the machine
Developing the hydraulics has been the backbone of the project. For three years the work followed a continuous cycle of design, testing and improvement, with multiple iterations combining simulation, laboratory testing and field analysis.
Every round pursued the same goal: gaining points of efficiency without giving up a millimetre of robustness. The result is a hydraulic design conceived to deliver high efficiency precisely where it is hardest to achieve.
3 years
Of intensive engineering work on the hydraulics
Design → test → improve
Multiple iterations until the target was reached
87.6%
Efficiency achieved on a certified test bench
Flow field simulation of the complete assembly
Project material · CFD
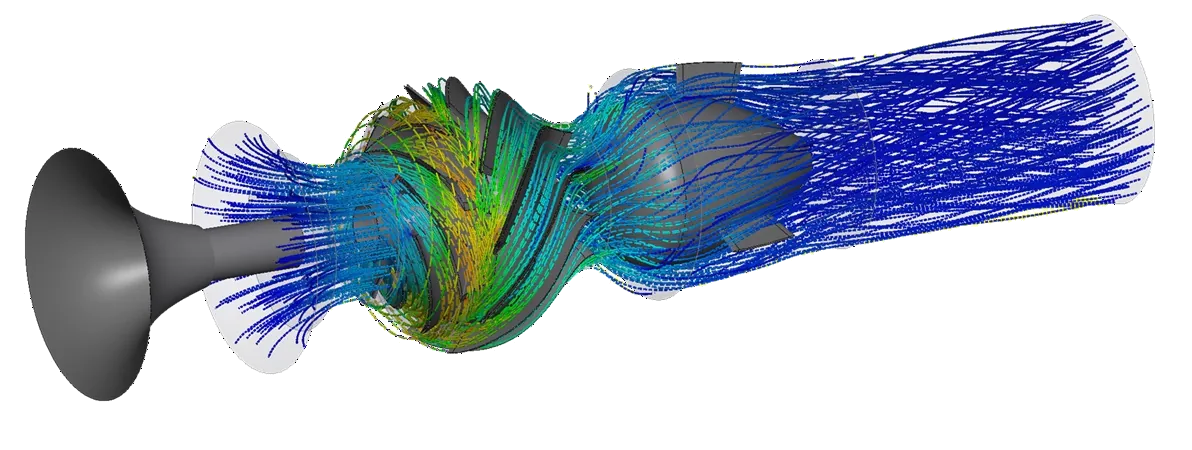
The streamlines, coloured by velocity, show how the water enters the impeller, how the diffuser collects it and where recirculation and losses appear. It is not just the impeller that is simulated: it is the whole assembly, because efficiency is lost as much in the vane as in what comes before and after it.
- Low velocity · inlet and outlet
- Medium velocity · diffuser
- High velocity · passage through the impeller
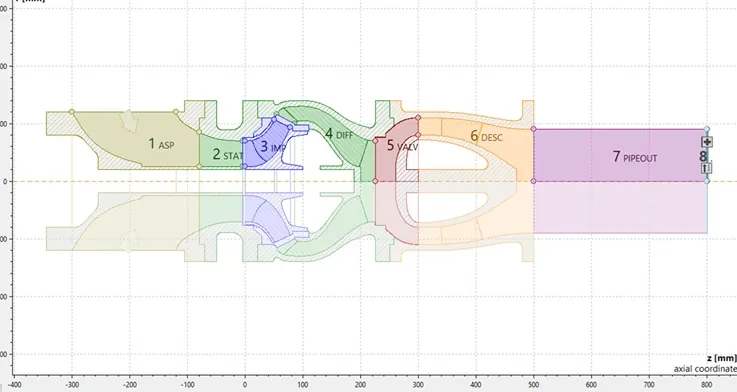
The meridional contour, section by section
Each section of the assembly (suction, stator, impeller, diffuser, valve, discharge and outlet pipe) is sized separately on the same contour and then checked again working together with the others.
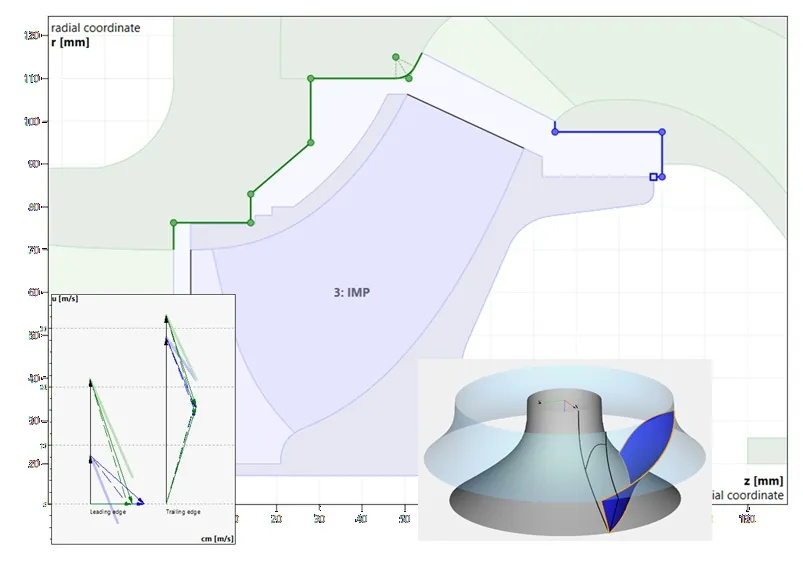
The vane angles, degree by degree
Velocity triangles at the leading edge and the trailing edge. The angles are adjusted so that the water enters and leaves the impeller without shock at the duty point: that is exactly where efficiency is won or lost.
This approach, based on real experimentation and not on calculation alone, is what has made it possible to comfortably exceed the efficiencies usual in the market, which lie between 75% and 80–82%.
02
High pressure capacity
Extreme conditions
as the starting point
One of the founding ideas of the project was to develop a pump capable of working in extreme conditions. Pressure is one of the most demanding: a machine installed at great depth has to withstand very high pressures permanently, not occasionally.
VITTA hydraulics are designed to withstand pressures of up to 70 bar, which allows pumping depths of up to 700 metres and significantly widens the machine’s range of application.
Working pressure
70 bar
Up to 700 m pumping depth
Thickness is calculated,
not estimated
Working at that pressure means sizing the structure accordingly. A detailed study was carried out of the thicknesses and strength of the structural components, determining in each area the thickness needed to withstand the load without compromising the integrity of the assembly.
Until there was
no weak area left
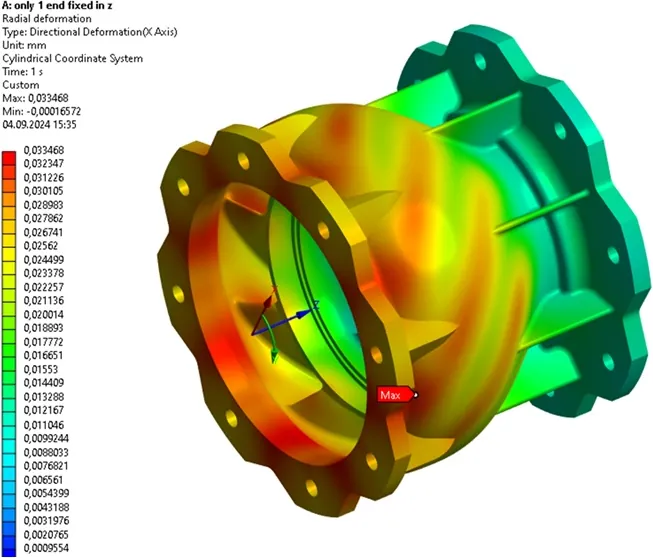
The first design did not hold. When it was subjected to the expected pressure conditions, the calculation showed areas of deformation and stress concentration that compromised the part. It had to be redesigned and recalculated, as many times as it took, until there were neither failure areas nor weak points left in the assembly.
Diffuser casing
Structural analysis
Before · Initial design
After · Validated design
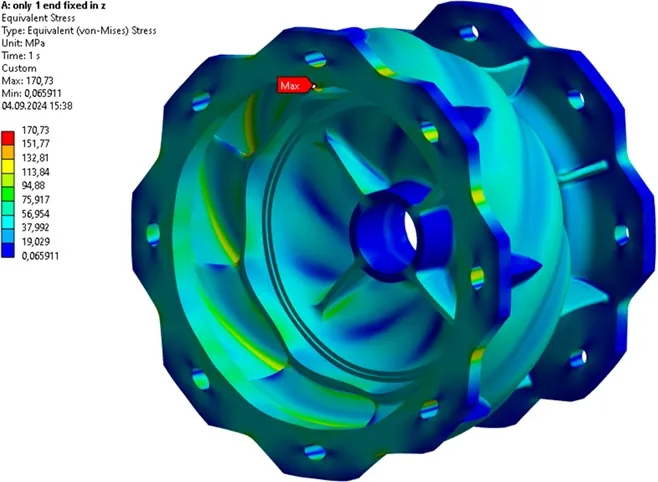
The redesign concentrated material where the calculation called for it, instead of spreading it evenly over the whole part.
Impeller
Structural analysis
Before · Initial design
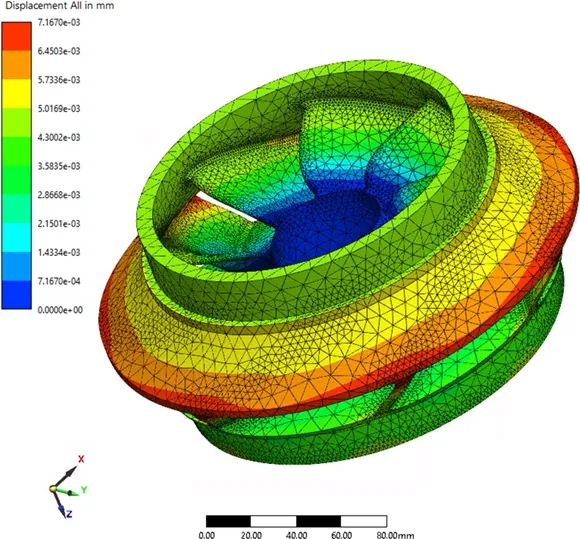
After · Validated design
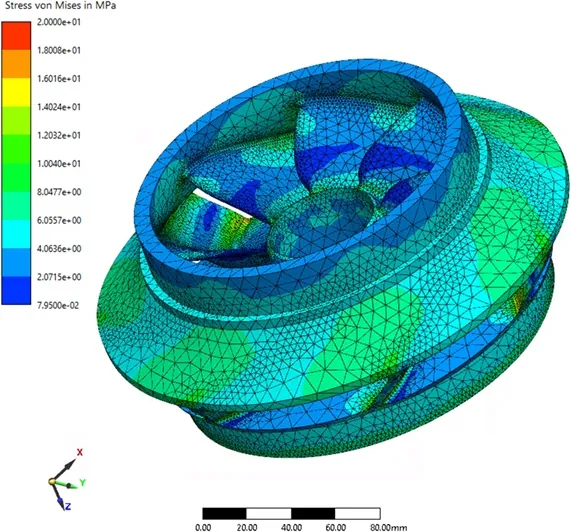
The mesh is refined where the load concentrates: that is where the thickness of each area is decided.
03
Reinforced structure
Robust on the
outside too
The internal design decides the efficiency. The exterior decides that the machine reaches the borehole in one piece, works for years and comes out of it in one piece.
These are pumps designed to lift water from great depth: coupled to high-power motors and with hydraulics of considerable length. That length, if the structure is not reinforced, ends up being a problem. And not only during normal operation: also during assembly, dismantling, transport and lifting.
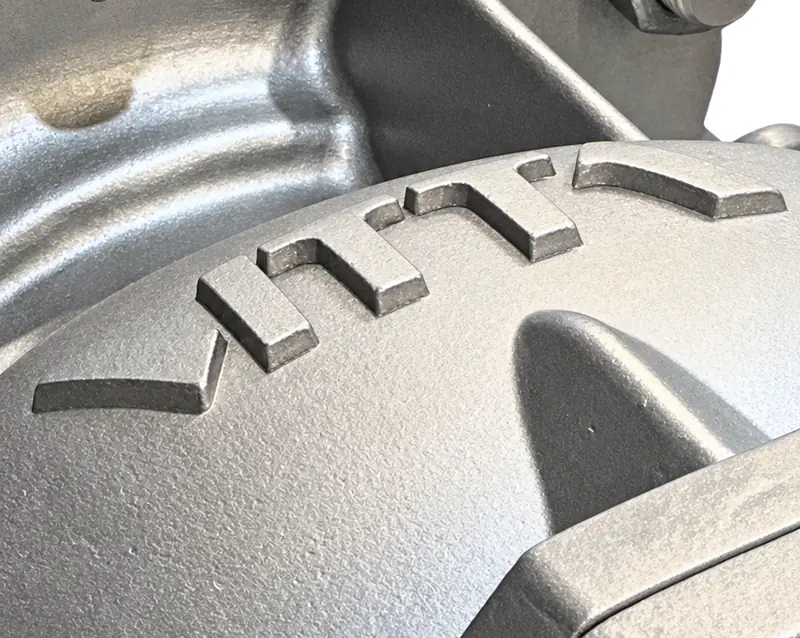
Reinforcing ribs on the outside
Robustness is not added afterwards: it comes in the very geometry of the cast part.
The critical point
The suction casing
In a submersible pump set, the suction casing sits roughly in the middle of the assembly, between the motor and the hydraulics. Because of its position and geometry, it is one of the weakest areas of a pump.
The most critical moment is lifting: the machine arrives on site horizontal and has to be stood upright. That is where it bears the greatest load and where, traditionally, it is most likely to break. Sixty years repairing equipment from every manufacturer have taught us exactly where it fails, and that is why it is one of the most heavily reinforced areas of a VITTA pump.
The same part solves something else: dedicated channels house the motor leads and keep them tucked away from the flow of water into the casing. If the water carries suspended solids, rust from the borehole, scale or sand, the cable insulation is protected from their impact. And since the cables run up recessed in their channel, they do not protrude from the profile of the machine: the outer diameter of the unit does not grow because of the cabling, which in narrow boreholes decides whether a pump fits or not.
Reinforcement and protection in the same part. Neither is noticed on the first day: they are noticed throughout the life of the machine.
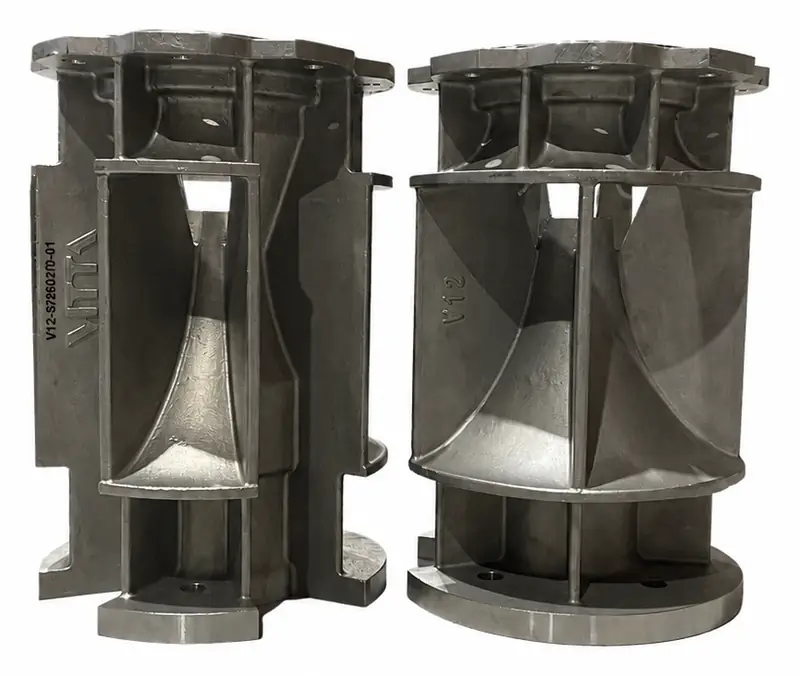
The reinforcement, in plain sight
Both decisions,
in the same part
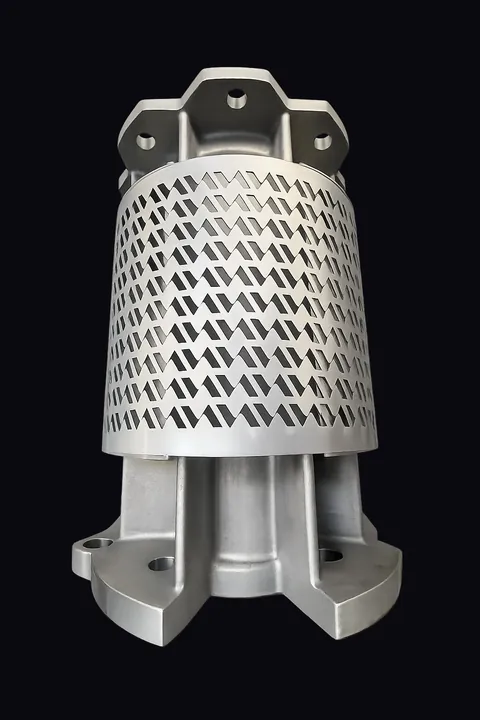
Two as-cast suction casings, side by side. On the left, the reinforcing gussets that join the flange to the body and spread the lifting load; on the right, the lengthwise channels that hold the motor cables.
Neither is added afterwards: both already come in the mould.
04
Casting quality
Investment casting: getting the design into the part intact
The hydraulics of the VITTA range are manufactured by investment casting, also known as lost-wax casting. It is a high-precision process that produces complex geometries with very tight tolerances and a high-quality surface finish.
It is neither the fastest nor the cheapest way to cast a part. It is the one that lets the hydraulic passage come out of the mould exactly as the design calculated it.
The process is the same for the two materials in which the range is manufactured: AISI 316 stainless steel in the standard version and super duplex for the most corrosive environments.
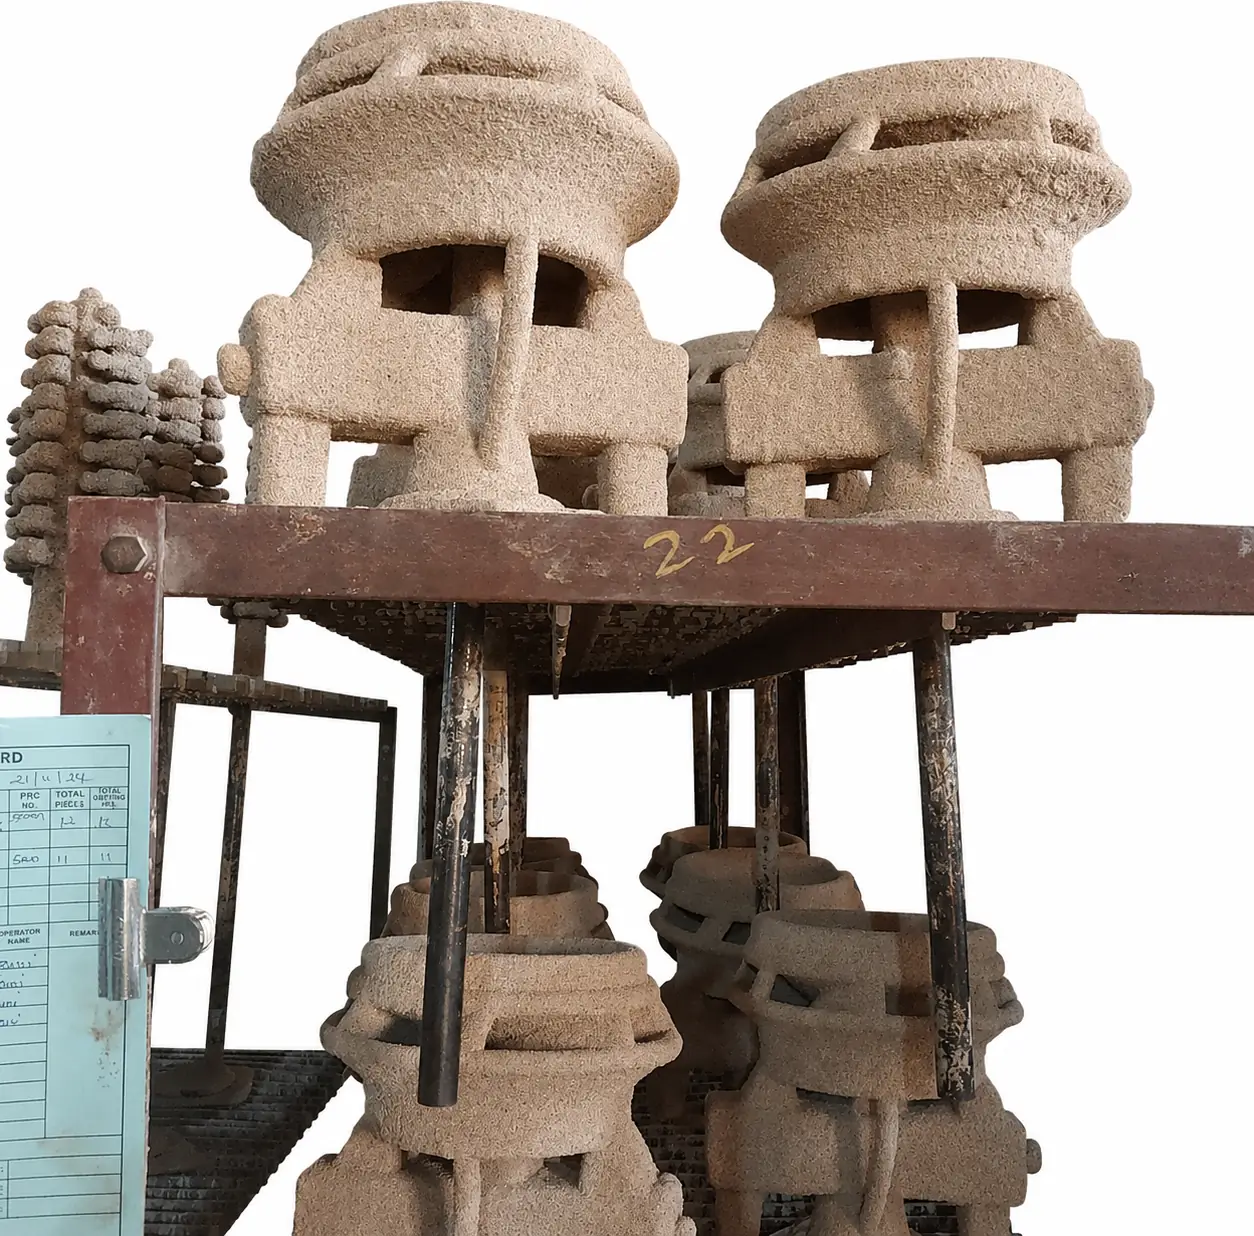
The process, step by step
01
Wax pattern
A wax pattern is made with the final geometry of the part.
02
Ceramic mould
The pattern is coated with layers of ceramic material until the mould is formed.
03
Dewaxing
Heat removes the wax and leaves the mould hollow, with the exact shape of the part.
04
Pouring
The mould is filled with molten metal: AISI 316 or super duplex, depending on the version.
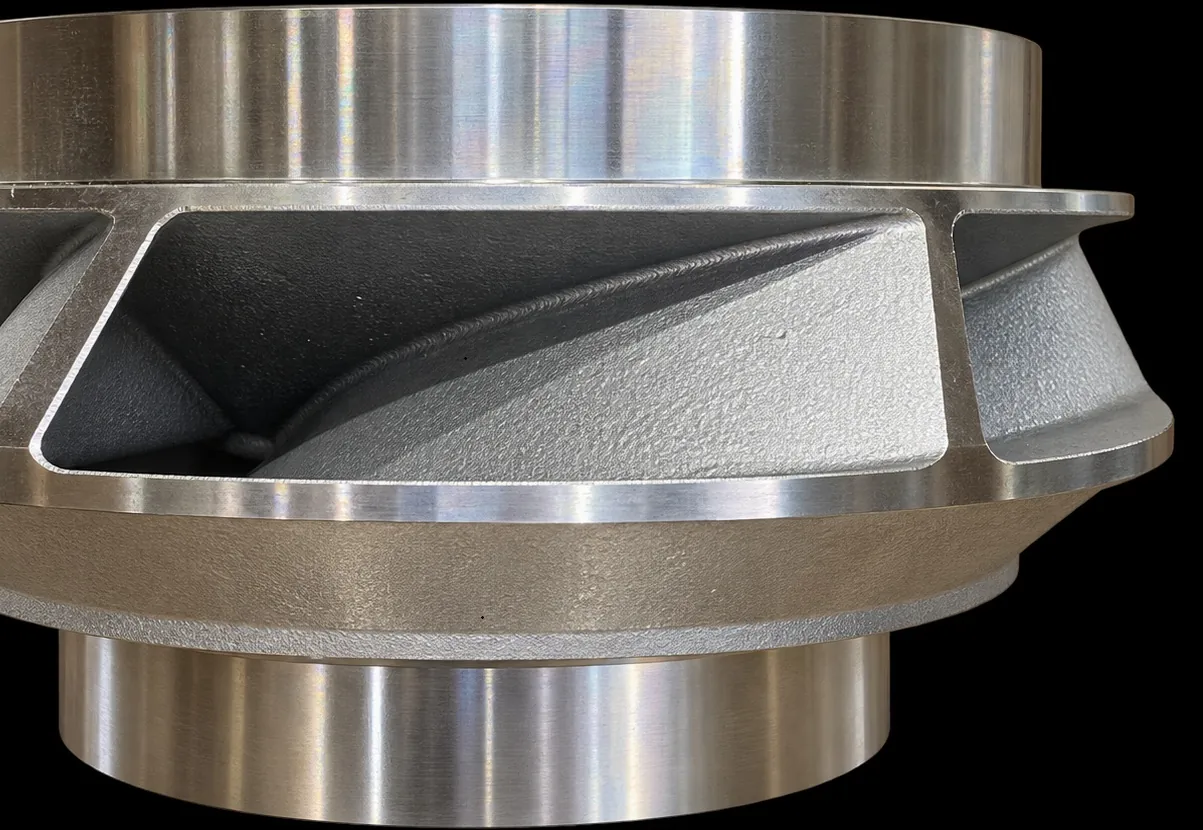
Close-up · as-cast finish
Section of a VITTA impeller. The evenness of the surface of the passage between vanes is a direct result of investment casting.
Why it matters
The finish decides the efficiency
The water that flows through an impeller passage loses energy through friction against the walls. The rougher the surface, the greater that loss. And once it has occurred, it is not recovered anywhere further along the machine.
That is why the finish is not a manufacturing detail: it is the condition for the efficiency calculated in the design to actually reach the pump.
An excellent geometry, cast with a poor finish, stops being excellent.
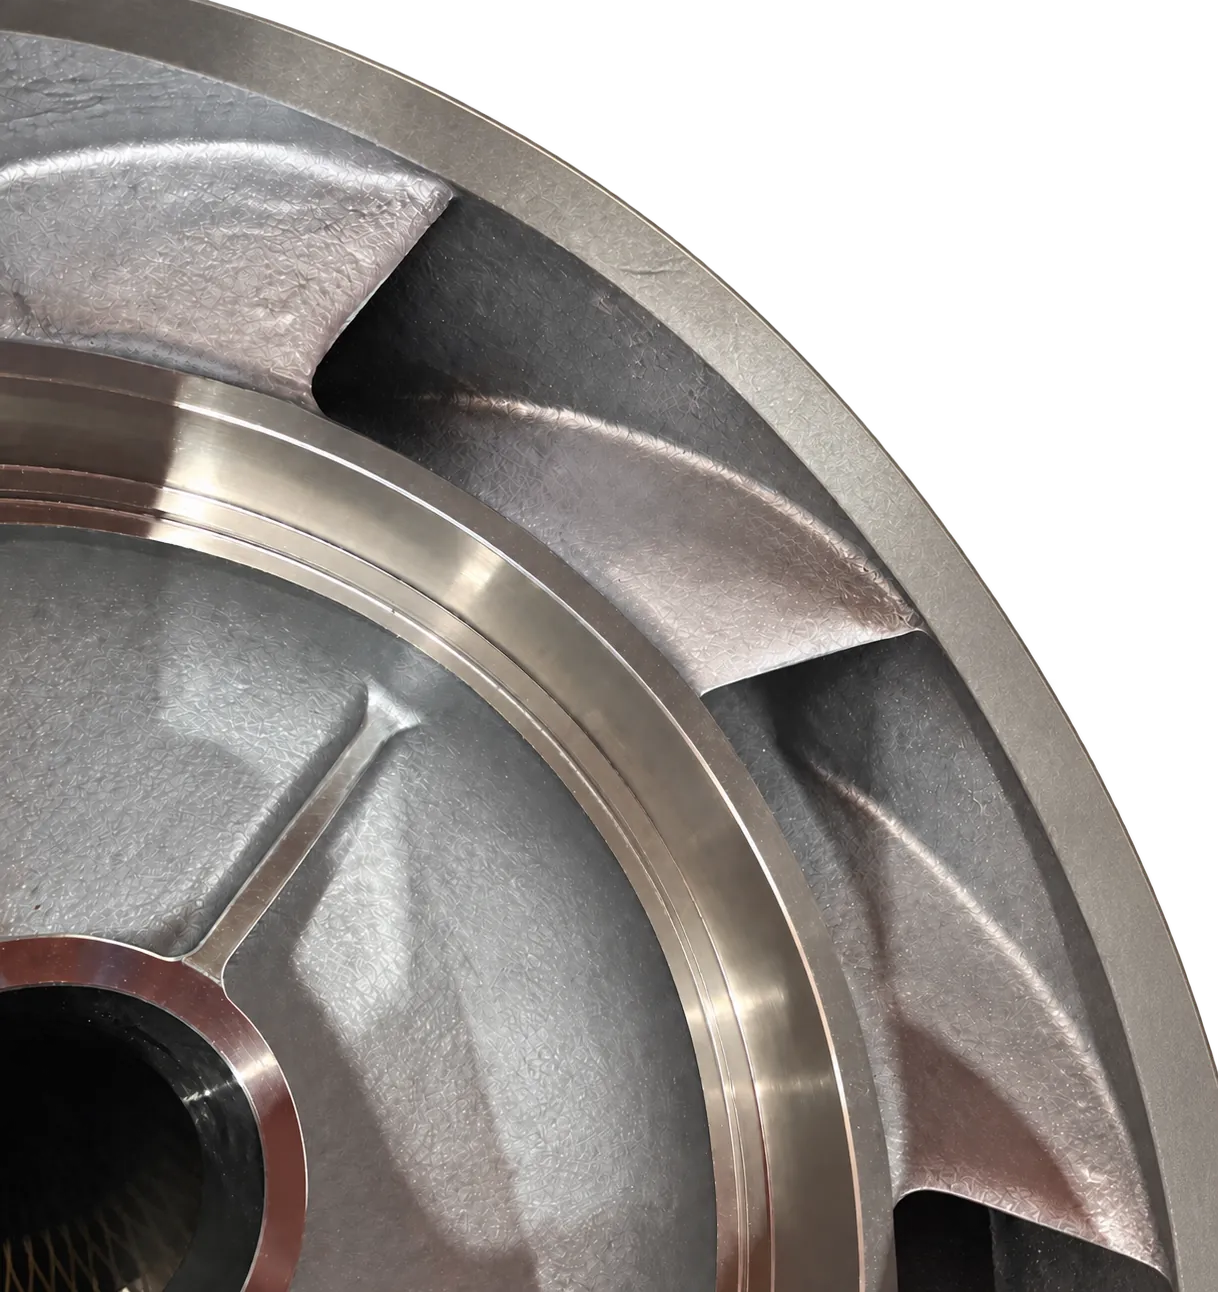
As-cast and machined surfaces
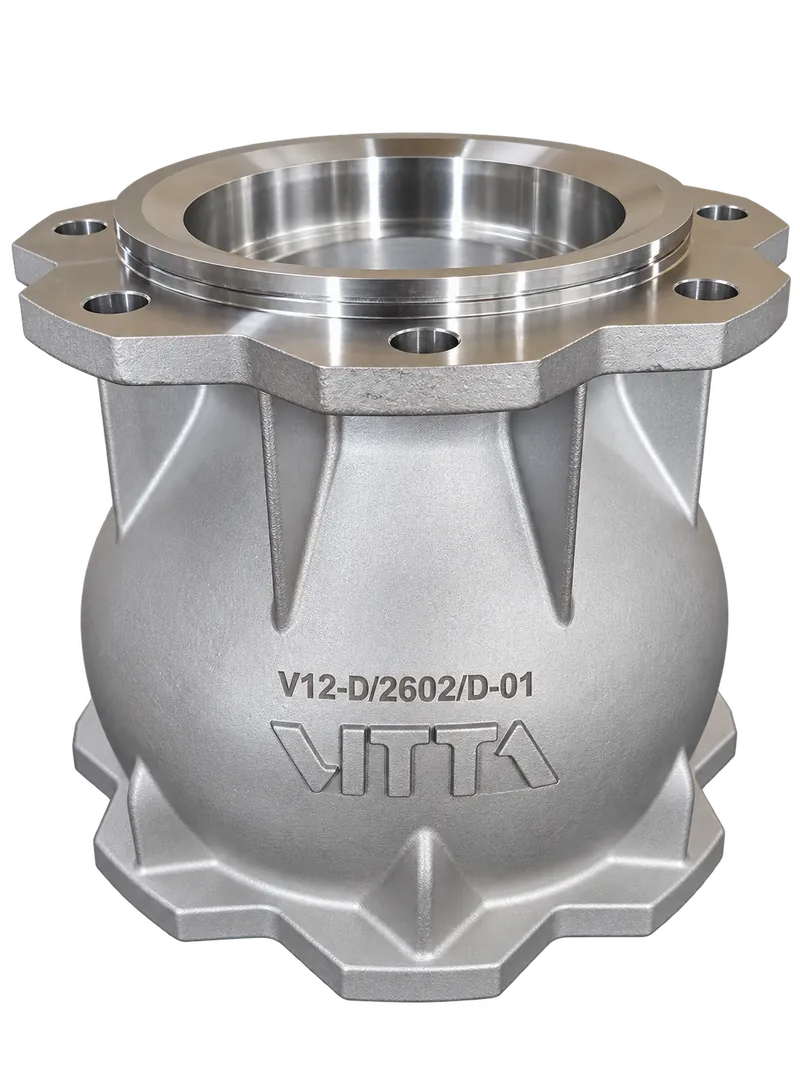
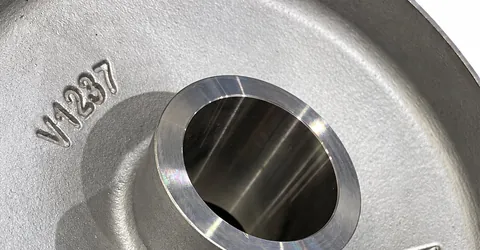
The surfaces that come out of the mould and the areas that are machined afterwards live side by side in the same part. The former are the ones the water sees.
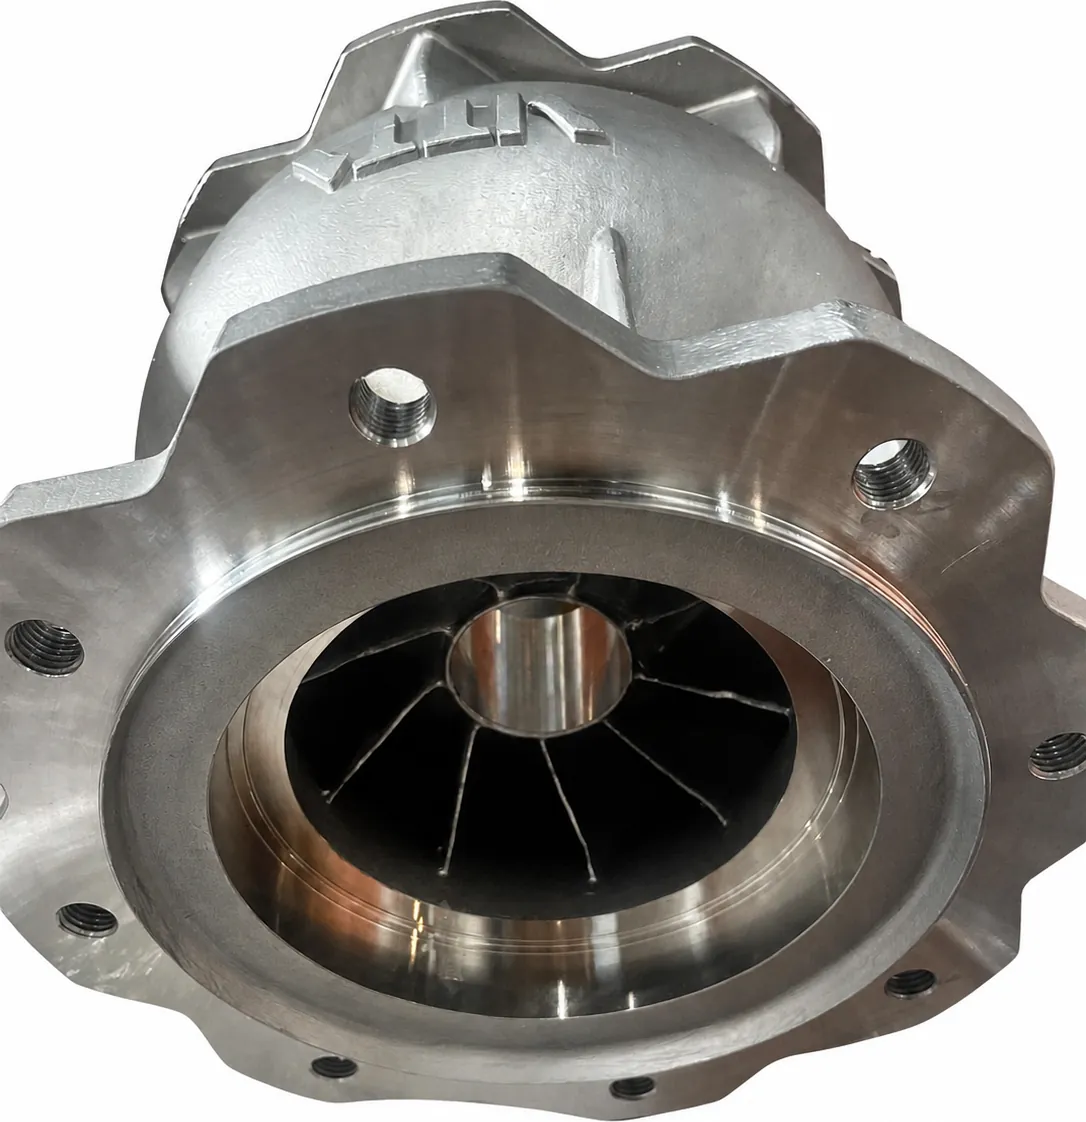
The marking comes from the mould
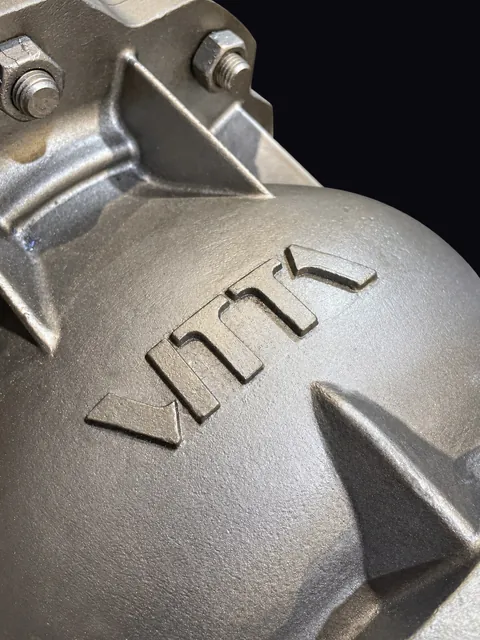
The VITTA name is produced in the casting itself; it is not added afterwards. In the background, the diffuser vanes just as they come out of the mould.
05
Quality control and traceability
Every part goes through
the same inspection
Reaching a high quality standard is half the job. The other half is making sure it does not slip over time. That is why every part and every component of a VITTA machine goes through the same strict inspection before assembly, unit by unit.
Once the parts arrive from the foundry, three things are checked: that the geometry is the one in the design, that the material is what it should be and that the machining is within tolerance. Once all three are passed, the part receives its serial number.
01
Dimensional verification by 3D scanning
Project material · Deviation report
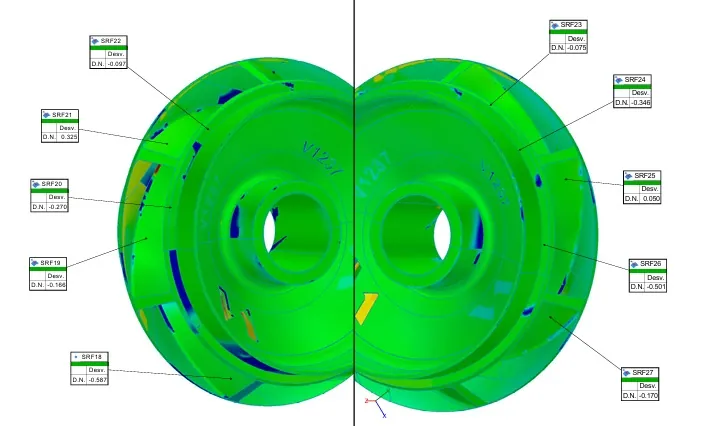
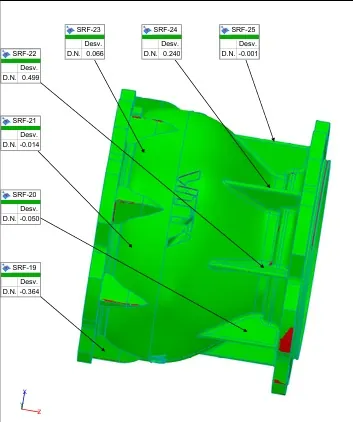
Each part is scanned and the result is compared with the original 3D design. The colour map shows the deviation point by point and the labels give the measurement on each control surface. This is how deviations in the mould or the casting are detected: before machining, not after assembly.
02
Material analysis
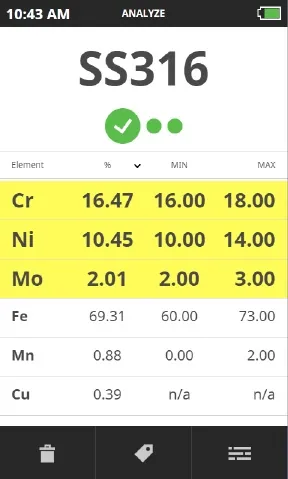
The composition of the alloy is analysed to confirm that the part is made of the right material. The instrument compares each element (chromium, nickel, molybdenum) with the range allowed for AISI 316 stainless steel.
The part is accepted only if all of them fall within range.
03
Machining inspection
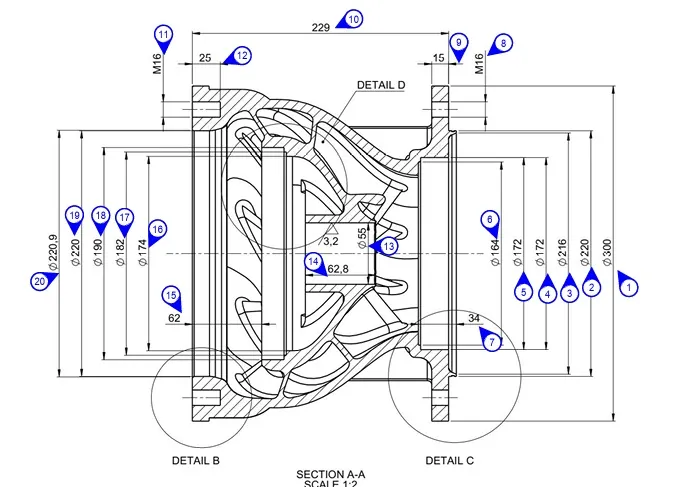
Once machining is finished, it is checked dimension by dimension against the drawing: diameters, lengths, threads and surface finishes. Each numbered dimension on the drawing is a verification point with its tolerance.
This is what ensures the correct assembly of the unit and the operation of the pump.
04
Serial number and traceability
Every part leaves with its own name
Once the three inspections are passed, the part receives its serial number: a unique serial reference that is marked on it, next to the VITTA name.
That reference is entered in the manufacturing record of the machine it is fitted to. Every pump set we supply has on record, part by part, which components it is made of and which inspections each one passed.
Years later, when it comes to an overhaul or a repair, nothing has to be guessed: it is written down.
What is guaranteed
Shape
The geometry is that of the original design.
Material
The alloy is the one specified and is within range.
Machining
All dimensions, within tolerance.
Identity
Serial number recorded in the machine's record.
06
Real-world and laboratory testing
Validated in the laboratory
and in service
First the bench. Then the borehole.
With the design finished, the project faced its most decisive phase: validating hydraulic efficiency and energy efficiency. It was tackled in a way that is unusual in the sector, structuring the tests on two levels.
A machine can perform very well in the laboratory and behave differently in a real borehole. That is why it was not considered validated until it had been checked in both situations.
Validation approach
Two levels
- Certified test bench
- Real operating conditions
How a VITTA is tested
If it is designed for extreme conditions, it is tested in demanding conditions
Tests on a multistage pump can be run with a reduced number of stages: that is the usual practice and it is much simpler. At VITTA we wanted to go further and carry out the validation with a high number of stages, to reproduce much more faithfully the configuration and conditions in which these pumps will later work.
The criterion was the same on the bench and in the borehole: test close to real operating conditions, not in the most comfortable scenario.
7 and 8 stages
Complete hydraulics in the bench tests, not individual stages
300–400 m
Test heads in the validation boreholes
600–800 hp
Power of the motors used in the tests
Level 01 · laboratory
Certified test bench
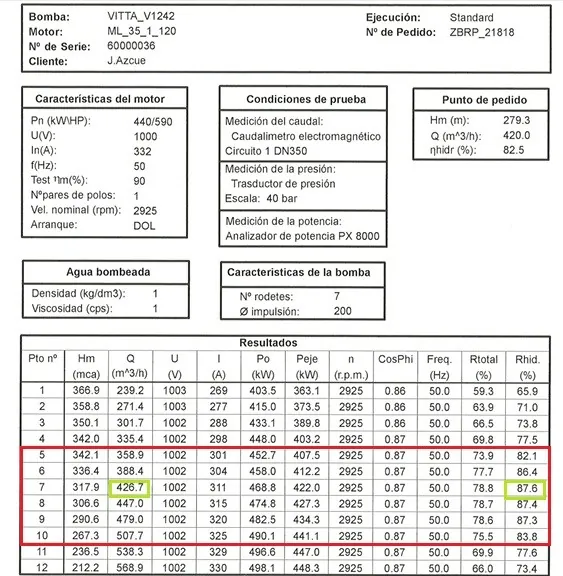
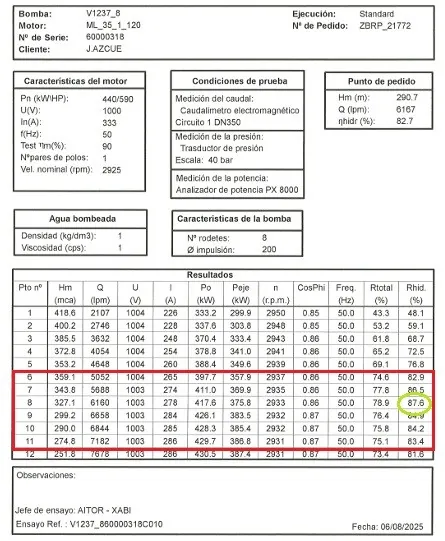
The validation tests were carried out on test benches of recognised European standing, under certified protocols.
Result: 87.6% hydraulic efficiency, recorded in the test reports.
Level 02 · in service
Real conditions
On a bench the conditions are ideal: clean water, stable temperature and a controlled environment. That is why, once the laboratory results were in, an additional step was taken that is uncommon at this stage of development: checking how the machines actually work in real boreholes.
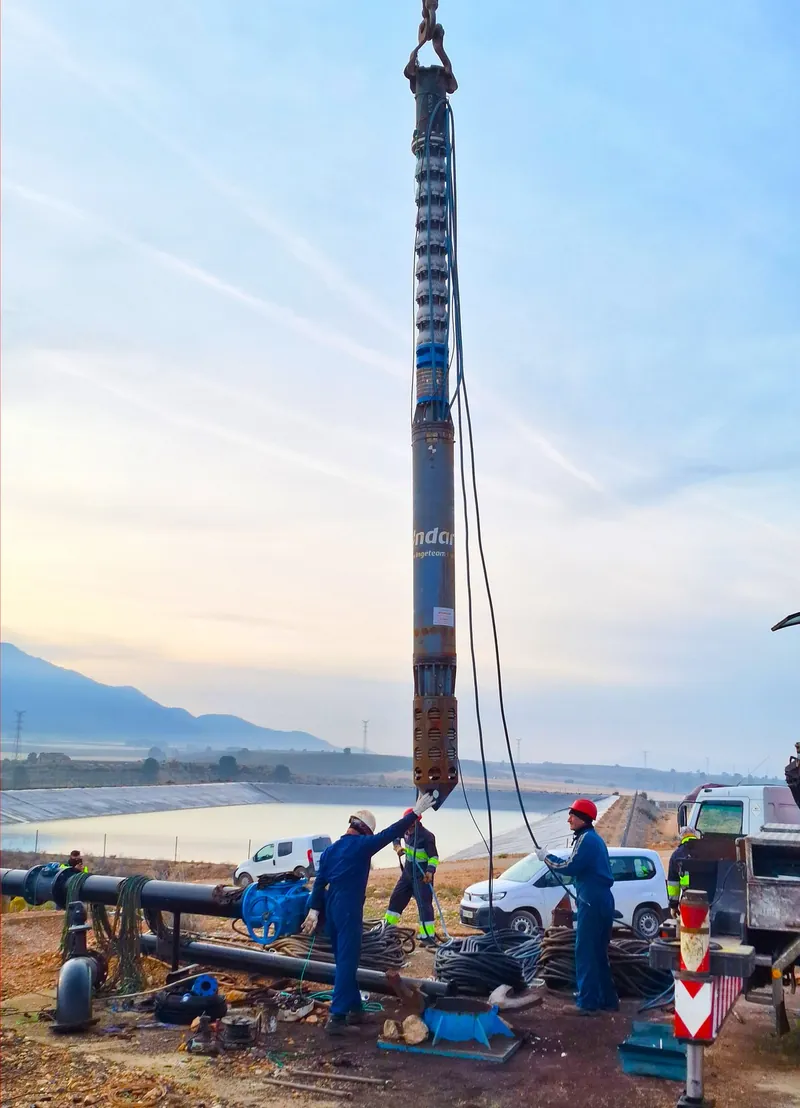
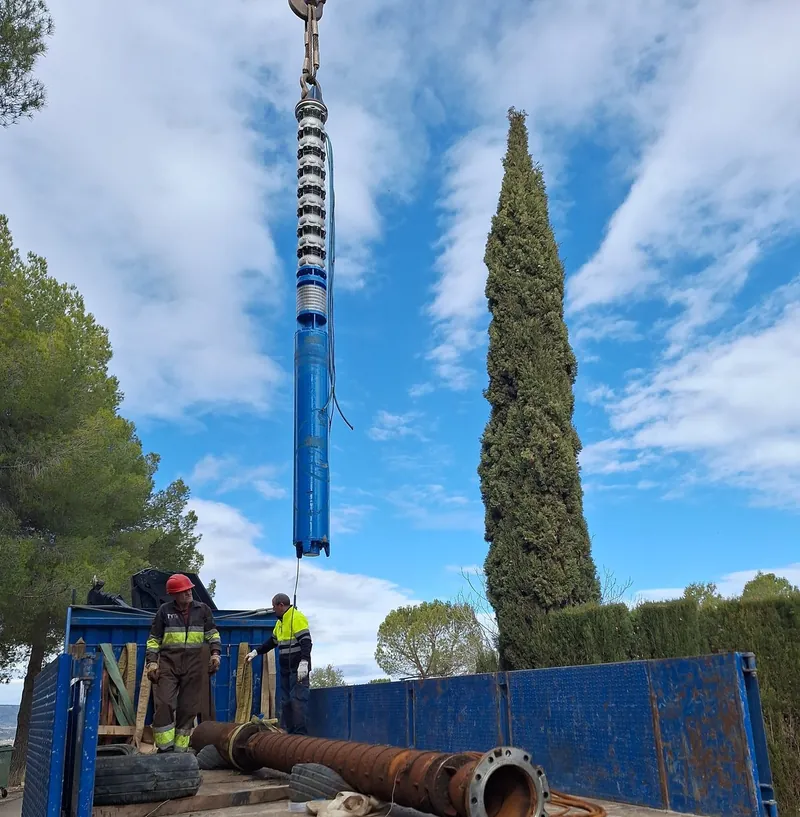
Thanks to the collaboration of customers, VITTA machines were installed in boreholes of 300 to 400 metres, with motors of 600 and over 800 hp.
Result: 86% hydraulic efficiency. At great depth the water is that of the aquifer and the column the pump supports is much greater: it is to be expected that the figure drops somewhat compared with the bench. What matters is how much it drops.
Two real cases
From the test to the customer's installation
Two boreholes in service with the same starting point: a machine that was already working and a limit the customer could not exceed. The real duty point was measured and the VITTA machine was selected for that point.
Case 01
Reducing power without losing flow
Installation · [ Data pending ]
The problem
The installation was drawing more than the 700 kW of contracted power. The customer needed to cut consumption while keeping the flow rate being extracted.
Tests
Measurement of the real duty point of the borehole (flow rate, dynamic water level and head losses) and comparison with the machine's bench curve.
Solution
Replacement of the pump set with a VITTA machine selected for that duty point.
Result
Extraction flow rate
126 L/s
Compared with the previous 118 L/s (+6.8%)
Power
−30 kW
Installation below the 700 kW contracted
Hydraulic efficiency in the field
85.56 %
Test bench: 87.4% (diff. < 2%)
Total head
345.5 m
Dynamic water level 334 m + 11.5 m of head losses
Case 02
More flow with the same power
Installation · [ Data pending ]
The problem
The customer needed to extract more flow from the borehole, but could not increase the installed power.
Tests
Measurement of the real duty point of the borehole and study of how the curve shifts as the dynamic water level varies.
Solution
VITTA machine selected to work within the power already available.
Result
Extraction flow rate
115 L/s
Compared with the previous 103 L/s (+11.7%)
Power
No increase
The same installed power, with no increase
Maximum expected efficiency
85.63 %
As the dynamic water level drops, the curve shifts towards the optimum
Total head
274.5 m
251 m + 15 m of head losses + 8.5 m of pressure
Catalogue decision
The VITTA catalogue publishes the real efficiency, not the bench figure
The usual practice in the sector is to publish the figure obtained in the laboratory, which is always the most favourable: clean water, stable temperature and a controlled environment.
At VITTA we have decided the opposite. The catalogue hydraulic efficiency is 85.6%, a figure sustained under real operating conditions and kept separate from the results obtained on the bench. What the customer reads is what the machine will deliver in their borehole.
87.6%
Measured on a certified bench
86%
Measured in the borehole, in service
85.6%
Catalogue hydraulic efficiency
[ Under construction ]
In-house hydraulic test bench
Juan Azcue is building its own hydraulic test bench. It will allow certified tests to be carried out in accordance with ISO 9906, guaranteeing the reliability and traceability of the results, and it is designed to simulate real operating conditions: not only hydraulic efficiency, but also the behaviour of the materials and the response of the machine in demanding working situations.
07
Passion for detail
It has to be
well made even if
nobody sees it
A borehole pump works hundreds of metres underground. Nobody sees it: not the person who buys it, not the person who irrigates with it, not the person who turns on the tap at the end of the network. It could be badly finished and, for years, nobody would find out.
We do not think that is right. A machine calculated for 70 bar, cast part by part and verified unit by unit deserves to be as well cared for on the outside as on the inside. The finish, the marking and the shape are worked on here to the same standard as the hydraulic efficiency.
Because whoever installs a VITTA has to know, just by looking at it, what they have in their hands.
The finished unit
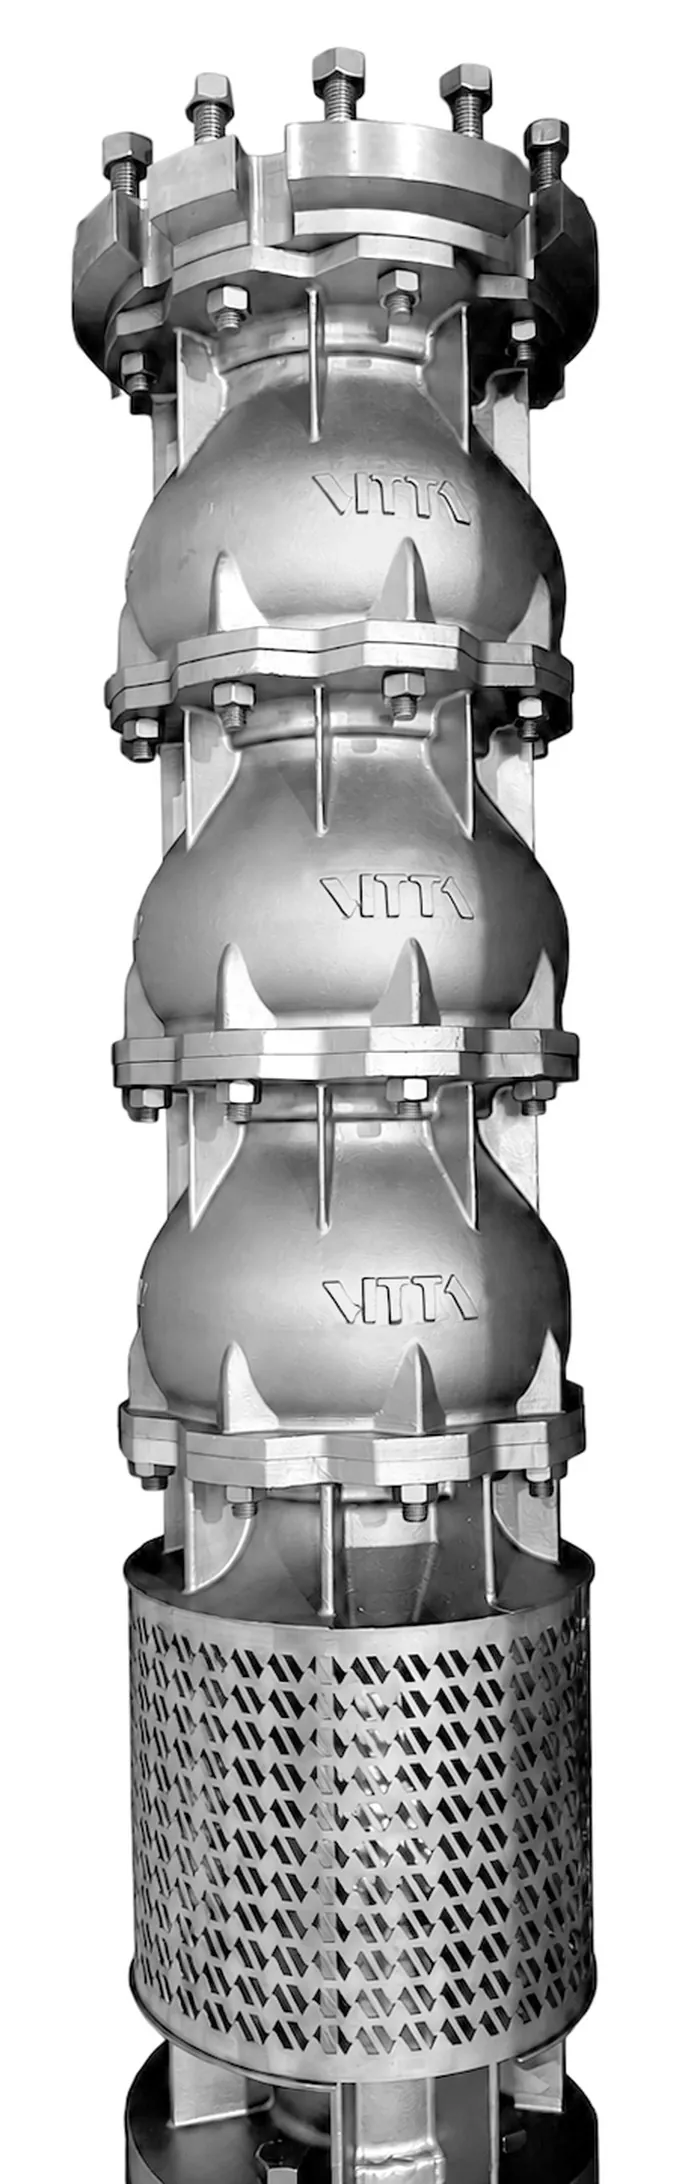
The complete
pump
Investment-cast stages, joined by their rosette flanges; the suction casing with its strainer; the marking and the serial number on every part. Everything the six previous sections describe, assembled and ready to go down the borehole.
Coupled to its motor, a pump set of this type easily exceeds five or six metres in length. It will work for years hundreds of metres underground, without anyone seeing it again until it is next pulled out.
And even so it is finished as if it were going to stay on display.
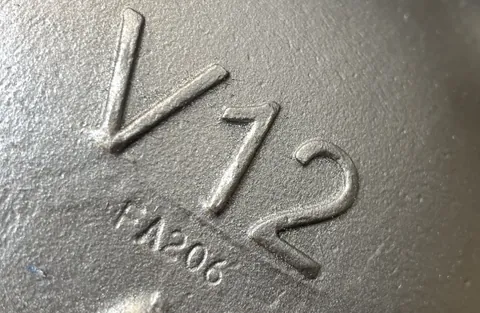
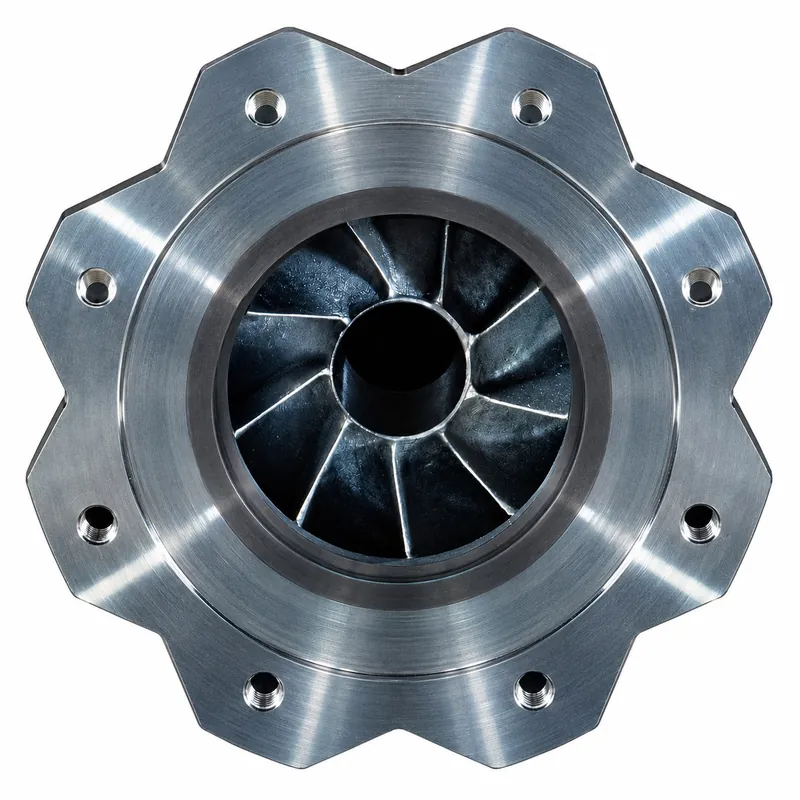
The shape
The rosette: recognisable from a distance, and useful too
We wanted a VITTA pump to be recognised from afar, without having to read anything. Hence the rosette shape of the discharge flange: it is the silhouette of the machine, and it is repeated across the whole range.
But it is not just shape. The recesses of the rosette act as channels for the motor’s power cables, which run up recessed in them instead of on the outside. The cabling does not protrude from the profile of the pump and the outer diameter of the unit does not grow because of it: in narrow boreholes, that decides whether a machine fits or not.
Recognisable shape and function solved in the same part. Neither is added afterwards: both already come in the mould.
Seven engineering decisions that cannot be seen from outside the borehole, and that are exactly what allow a machine to maintain 86% efficiency working at a depth of 400 metres.